

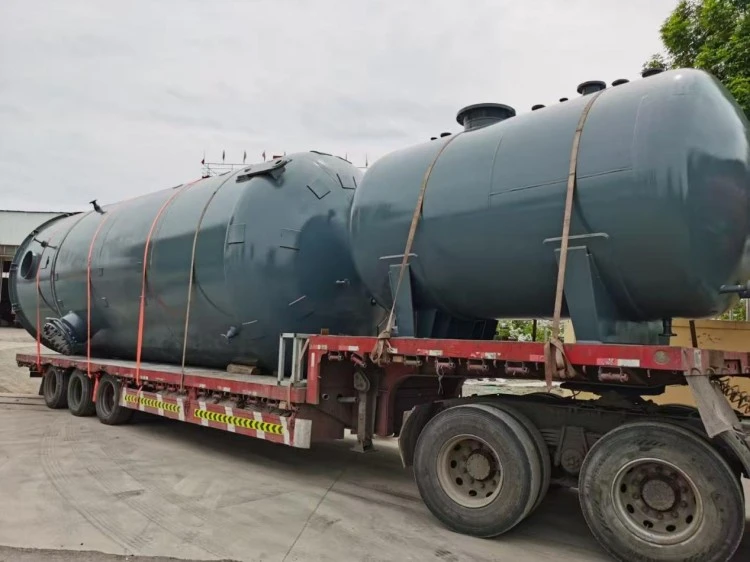
This series of reflux drums is designed and manufactured according to pressure vessel standards such as ASME and GB/T, and the design calculations are based on reverse engineering principles considering the condenser load at the top of the column, the range of reflux ratio variations, and the proportion of non-condensable gases.
The tank body is equipped with a buffer and flow stabilization structure and a gas-liquid secondary separation component to ensure that the liquid entering the reflux pump has a stable density and low gas content.
product Advantages
More stable reflux ratio, easier to meet cutting specifications
More stable reflux pump suction
Significantly reduced reflux ratio fluctuations
Easier to consistently meet product cutting point specifications
Prevents pump cavitation, extending equipment life
By precisely calculating the minimum safe liquid level and pump suction inlet elevation, the reflux pump is ensured to operate under liquid-sealed conditions for extended periods, reducing the incidence of cavitation, vibration, and frequent pump shutdowns, significantly extending the life of the pump and seals.
Balances non-condensable gas discharge and system safety
An independent non-condensable gas discharge channel and pressure buffer are provided to prevent gas accumulation from causing artificially high liquid levels or control distortion, resulting in a more accurate and easier-to-adjust tower top control system.
Internal anti-fouling structure, reducing maintenance frequency
The large-channel internal component structure and low-retention zone design reduce the likelihood of wax buildup, scaling, and sedimentation,
significantly extending the continuous operating cycle of the reflux system.


Industry Applications
Atmospheric and vacuum distillation columns, reflux systems
Fractionation sections of hydrotreating, aromatization, and cracking units
Continuous separation systems in fine chemical processes
Benefits after implementation in these industries

Customization Options
Size determined by backflow rate, condensation load, and non-condensable gas ratio
Material: Q345R / Stainless Steel / Duplex Steel
Customizable internal structure, interface orientation, and instrument ports
Integrated insulation, heat tracing, and corrosion protection
Technical Support
Our technical support is not simply answering questions, but rather a collaborative engineering service that spans the entire project lifecycle, ensuring that every step of the Reflux Tank project, from "design" to "stable operation," is problem-free.
Design and Selection Phase Support
Performing reverse engineering calculations based on reflux flow rate, reflux ratio range, overhead condenser load, and non-condensable gas ratio.
Assisting in calculating minimum safe liquid level, pump suction inlet elevation, and gas-liquid separation efficiency.
Providing optimization suggestions for tank structure, internal components, and interface layout.
Avoiding frequent modifications later due to improper selection.
Manufacturing and Acceptance Phase Support
Providing manufacturing process instructions, critical weld inspection, and material traceability documents.
Cooperating with third-party and owner acceptance (ITP, FAT).
Completing internal structure pre-assembly and dimensional verification before shipment.
Ensuring "direct placement and no rework" during on-site installation.
Installation and Commissioning Phase Support
Providing lifting point drawings and installation sequence suggestions.
Guiding the correct connection of level gauges, vents, and reflux inlets.
Providing suggestions for initial operation reflux ratio and liquid level stability parameter ranges.
Avoiding situations where the system is "installed correctly but doesn't run well."
Operation and Optimization Support
Providing long-term stability diagnostic suggestions for the reflux system.
Guiding troubleshooting of abnormalities such as scaling, cavitation, and liquid level drift.
Supporting structural assessment for capacity expansion and increased load operation.
Truly achieving: We don't disappear after the sale; the project has long-term support.

If you are looking for a more stable, less prone to failure, and easier-to-adjust reflux system for your tower system,
please submit your tower top operating conditions, and we will design the optimal reflux drum solution for you.
Hot Tags: reflux tank, China reflux tank manufacturers, suppliers, factory, Atmospheric Tank, chem tanks, used chemical tanks, tank chemical, chemical tanks, Reflux Tank


